「Hytrel」:修訂間差異
跳至導覽
跳至搜尋
新頁面: ==押出注意事項== *參考Hytrel Extrusion Manual *押出前需乾燥,使其含水率低於0.08% (P3 Dyer) *L/D=24 以上(P3 Extruder barrel) *壓縮比 2.5~3.5(P3 Screw design)[... |
|||
| 第6行: | 第6行: | ||
*單螺桿(P3 Materials of construction) | *單螺桿(P3 Materials of construction) | ||
**約等長的三段設計(供料.壓縮.計量) | **約等長的三段設計(供料.壓縮.計量) | ||
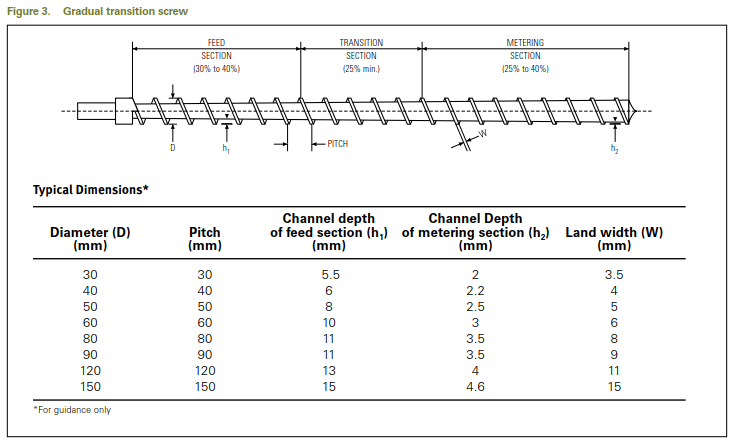
**For most Hytrel® extrusion purposes good results are obtained with simple 3-zone screws, having approximately equal length feed, transition (compression) and metering sections. The length-to-diameter (L/D) ratio should be ideally 24:1 or higher for good uniformity of extrudate (i.e., minimum temperature and | **For most Hytrel® extrusion purposes good results are obtained with simple 3-zone screws, having approximately equal length feed, transition (compression) and metering sections. The length-to-diameter (L/D) ratio should be ideally 24:1 or higher for good uniformity of extrudate (i.e., minimum temperature and pressure variations). Compression ratios should be between 2.5 and 3.5:1, as determined by the depth of feed zone channel divided by the depth of metering zone channel (“apparent compression ratio”) for constant pitch screws. The depth of channel in both feed and metering sections is important: if the | ||
pressure variations). Compression ratios should be between 2.5 and 3.5:1, as determined by the depth of feed zone channel divided by the depth of metering zone channel (“apparent compression ratio”) for constant pitch screws. The depth of channel in both feed and metering sections is important: if the | |||
feed channel is too deep and not sufficiently long, particularly with large diameter screws, it can cause poor feeding and irregular output with some harder Hytrel® types. | feed channel is too deep and not sufficiently long, particularly with large diameter screws, it can cause poor feeding and irregular output with some harder Hytrel® types. | ||
https://dl.dropboxusercontent.com/s/1vfk1d5002yd8t7/PDFXEdit_2016-08-19_09-49-46.png | https://dl.dropboxusercontent.com/s/1vfk1d5002yd8t7/PDFXEdit_2016-08-19_09-49-46.png | ||
於 2016年8月19日 (五) 09:50 的修訂
押出注意事項
- 參考Hytrel Extrusion Manual
- 押出前需乾燥,使其含水率低於0.08% (P3 Dyer)
- L/D=24 以上(P3 Extruder barrel)
- 壓縮比 2.5~3.5(P3 Screw design)螺桿LD比、壓縮比
- 單螺桿(P3 Materials of construction)
- 約等長的三段設計(供料.壓縮.計量)
- For most Hytrel® extrusion purposes good results are obtained with simple 3-zone screws, having approximately equal length feed, transition (compression) and metering sections. The length-to-diameter (L/D) ratio should be ideally 24:1 or higher for good uniformity of extrudate (i.e., minimum temperature and pressure variations). Compression ratios should be between 2.5 and 3.5:1, as determined by the depth of feed zone channel divided by the depth of metering zone channel (“apparent compression ratio”) for constant pitch screws. The depth of channel in both feed and metering sections is important: if the
feed channel is too deep and not sufficiently long, particularly with large diameter screws, it can cause poor feeding and irregular output with some harder Hytrel® types.